GTR Composites Group cuts chassis setup time by 66% with MSP’s CNC metrology software
At a glance
GTR, a leader in composite component manufacture, is now meeting increased customer demands for tighter tolerances and more complex work following the introduction of MSP PerfectPart. The technology has become integral to recent projects and now forms part of GTR’s USP, helping to demonstrate both consistency and quality of supply. In addition, MSP’s CNC metrology solutions have delivered measurable benefits to GTR including, a reduction in part setup time of 10 hours per part, along with the early detection of machine errors, to ensure repeatable right-first-time machining.
reduction in part setup time
This reduction in time, coupled with setup repeatability, means GTR has been able to meet customers' tight deadlines.
CNC machine capacity
MSP PerfectPart, has enabled GTR to bring work in-house and avoid the risk of managing an external supply chain.
confidence across the shopfloor
MSP PerfectPart's data gives reassurance that processes are correct. It is a game-changer for GTR's chassis setup.
Products used
Background
Leading composite component manufacturer, GTR Composites Group (GTR), has a strong heritage in motorsport and automotive part production, following work on IndyCar chassis for winning cars in the 90s. The company now supplies directly into companies across the defence, aerospace and marine industries, offering concept to component services via an experienced technical team.
GTR’s dedication to maintaining its impressive record of delivering quality components to tight deadlines led them company to approach MSP after recognising a shift in customer demand and higher expectations for chassis production.
Steven Davis, GTR Lead Machine Shop Engineer, says: “We are increasingly seeing tighter tolerances and customers asking for parts that, even if you went back five years, would have been impossible to machine”. “The expectation has gone crazy in the pursuit of perfect lap times. The accuracy of the chassis directly affects how the car performs on the track and, ultimately, that all boils down to how we set up and machine it”.
Challenge
GTR prides itself on delivering a complete end-to-end solution, from design through to delivery, including laminating, trimming, assembly and both pre- and post machining processes. With involvement throughout, GTR has a strong understanding of what it takes to produce a finished article, and the responsibility that comes with it.
As part and process complexity started to increase, GTR began to look at areas where machining accuracy could be improved. One of the primary focus areas was the part setup process due to manual involvement. The team were taking the traditional approach of manually setting up the part on the machine and making incremental adjustments to fine-tune the alignment.
“We were shimming and knocking fixtures around to get the part close to where it needed to be”, GTR’s Group Business & Operations Development Manager, Tom Hay, explains. “It was a labour-intensive process and it could take up to 15 hours to achieve a vaguely decent setup”.
Achieving the required level of setup accuracy was particularly time-consuming due to part deformation from the mould. Steven details: “The nature of moulded parts means they never come out exactly as you expect. The usual tolerance is anywhere between 0.3 and 0.5 millimetres of deflection on the moulded surfaces. When you factor those deflections into a part that’s 3 metres long, the front or rear end could be out by a millimetre or more”.
This deviation was often only becoming apparent within the machining results as Steven recalls:
“We could set up a chassis and think everything looked acceptable but then the results would come back and it wasn’t good news. When you’ve already spent hours on it, that’s pretty soul-destroying”.
Steven Davis, GTR Lead Machine Shop Engineer
A secondary factor affecting results was uncertainty around machine performance. Steven says: “We would follow the industry’s default approach - there’s no issue with the machine unless parts start to come out wrong. It was a purely reactive process and we relied on the annual service to keep everything steady”.
This was compounded by changing shopfloor conditions. Tom remarks: “Temperature through the machine can change quite drastically across seasons and this directly impacts the repeatability of components. If we machine the same part at different times of the year, we’re going to get a completely different result”.
With increasing customer pressure and tightening deadlines, these challenges became more significant and prompted GTR to focus on advancing processes and eliminating human error.
Steven comments: “Everything’s always wanted yesterday, especially within the motorsport sector. We knew that if we could get our machining right each time that would be half the effort done straight away”. Tom agrees and adds: “We were feeling the challenge of remaining competitive in an industry where innovation is at an all-time high, but processes are still very labour heavy”.
“On high-risk projects we want to know we’re doing as much as we can to iron out any issues, especially the human factor. However, there’s only so much you can do with internal processes alone. At some point you have to invest in the right software or equipment to move forward”.
Solution
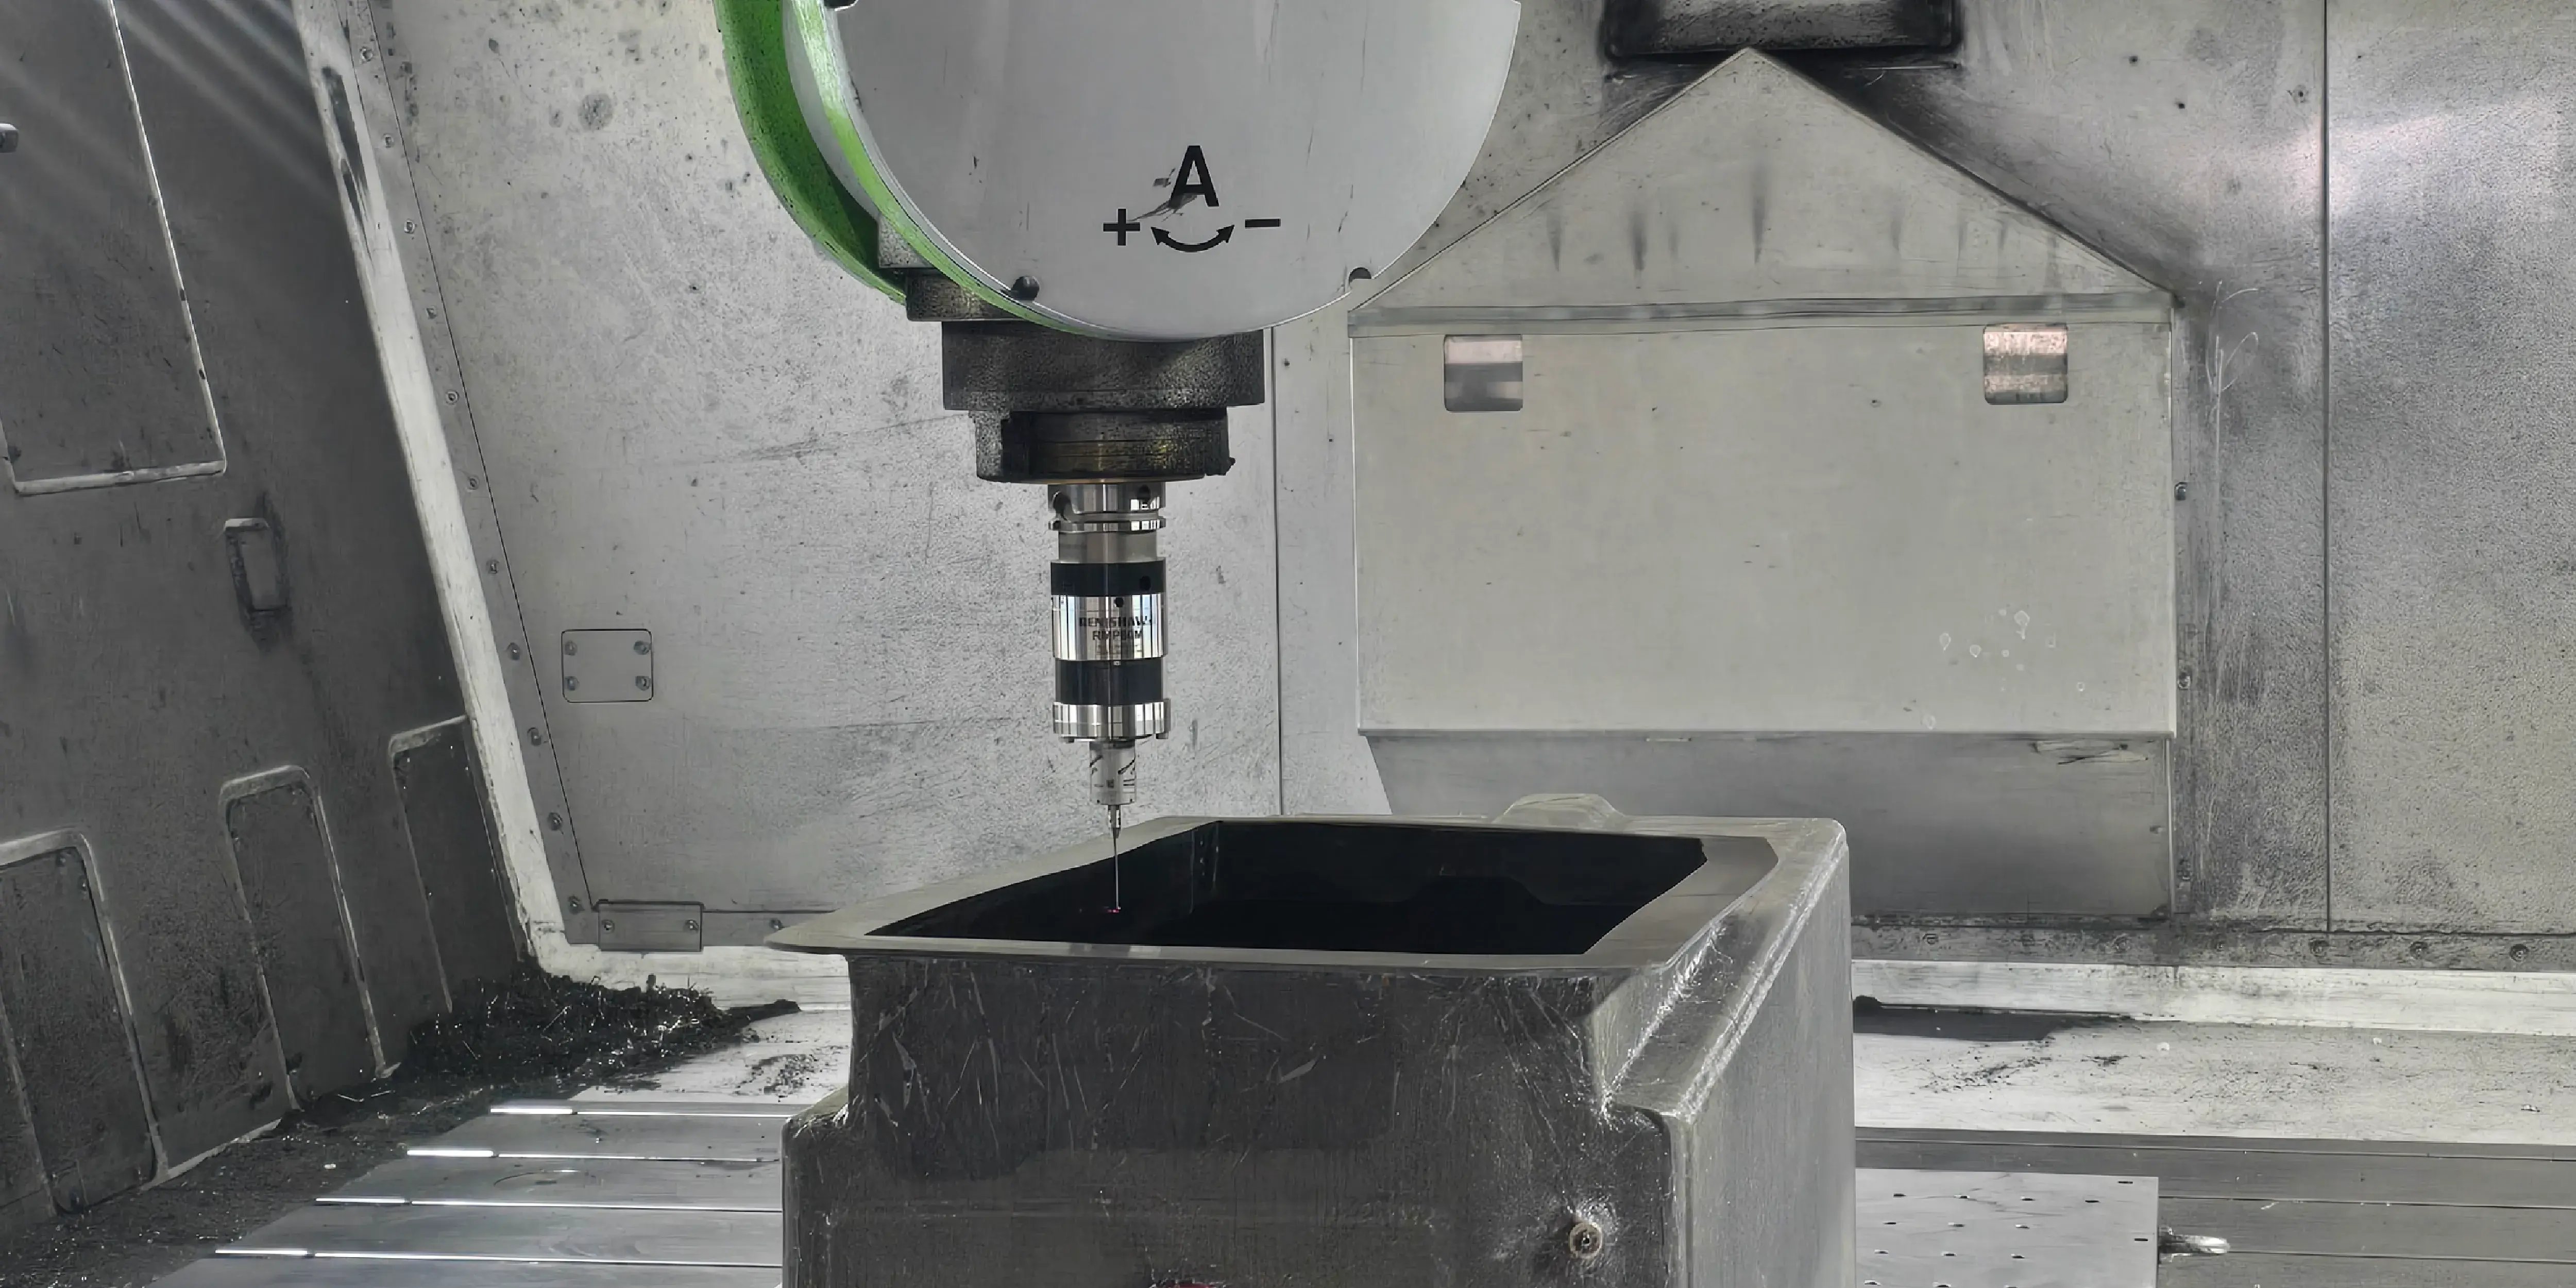
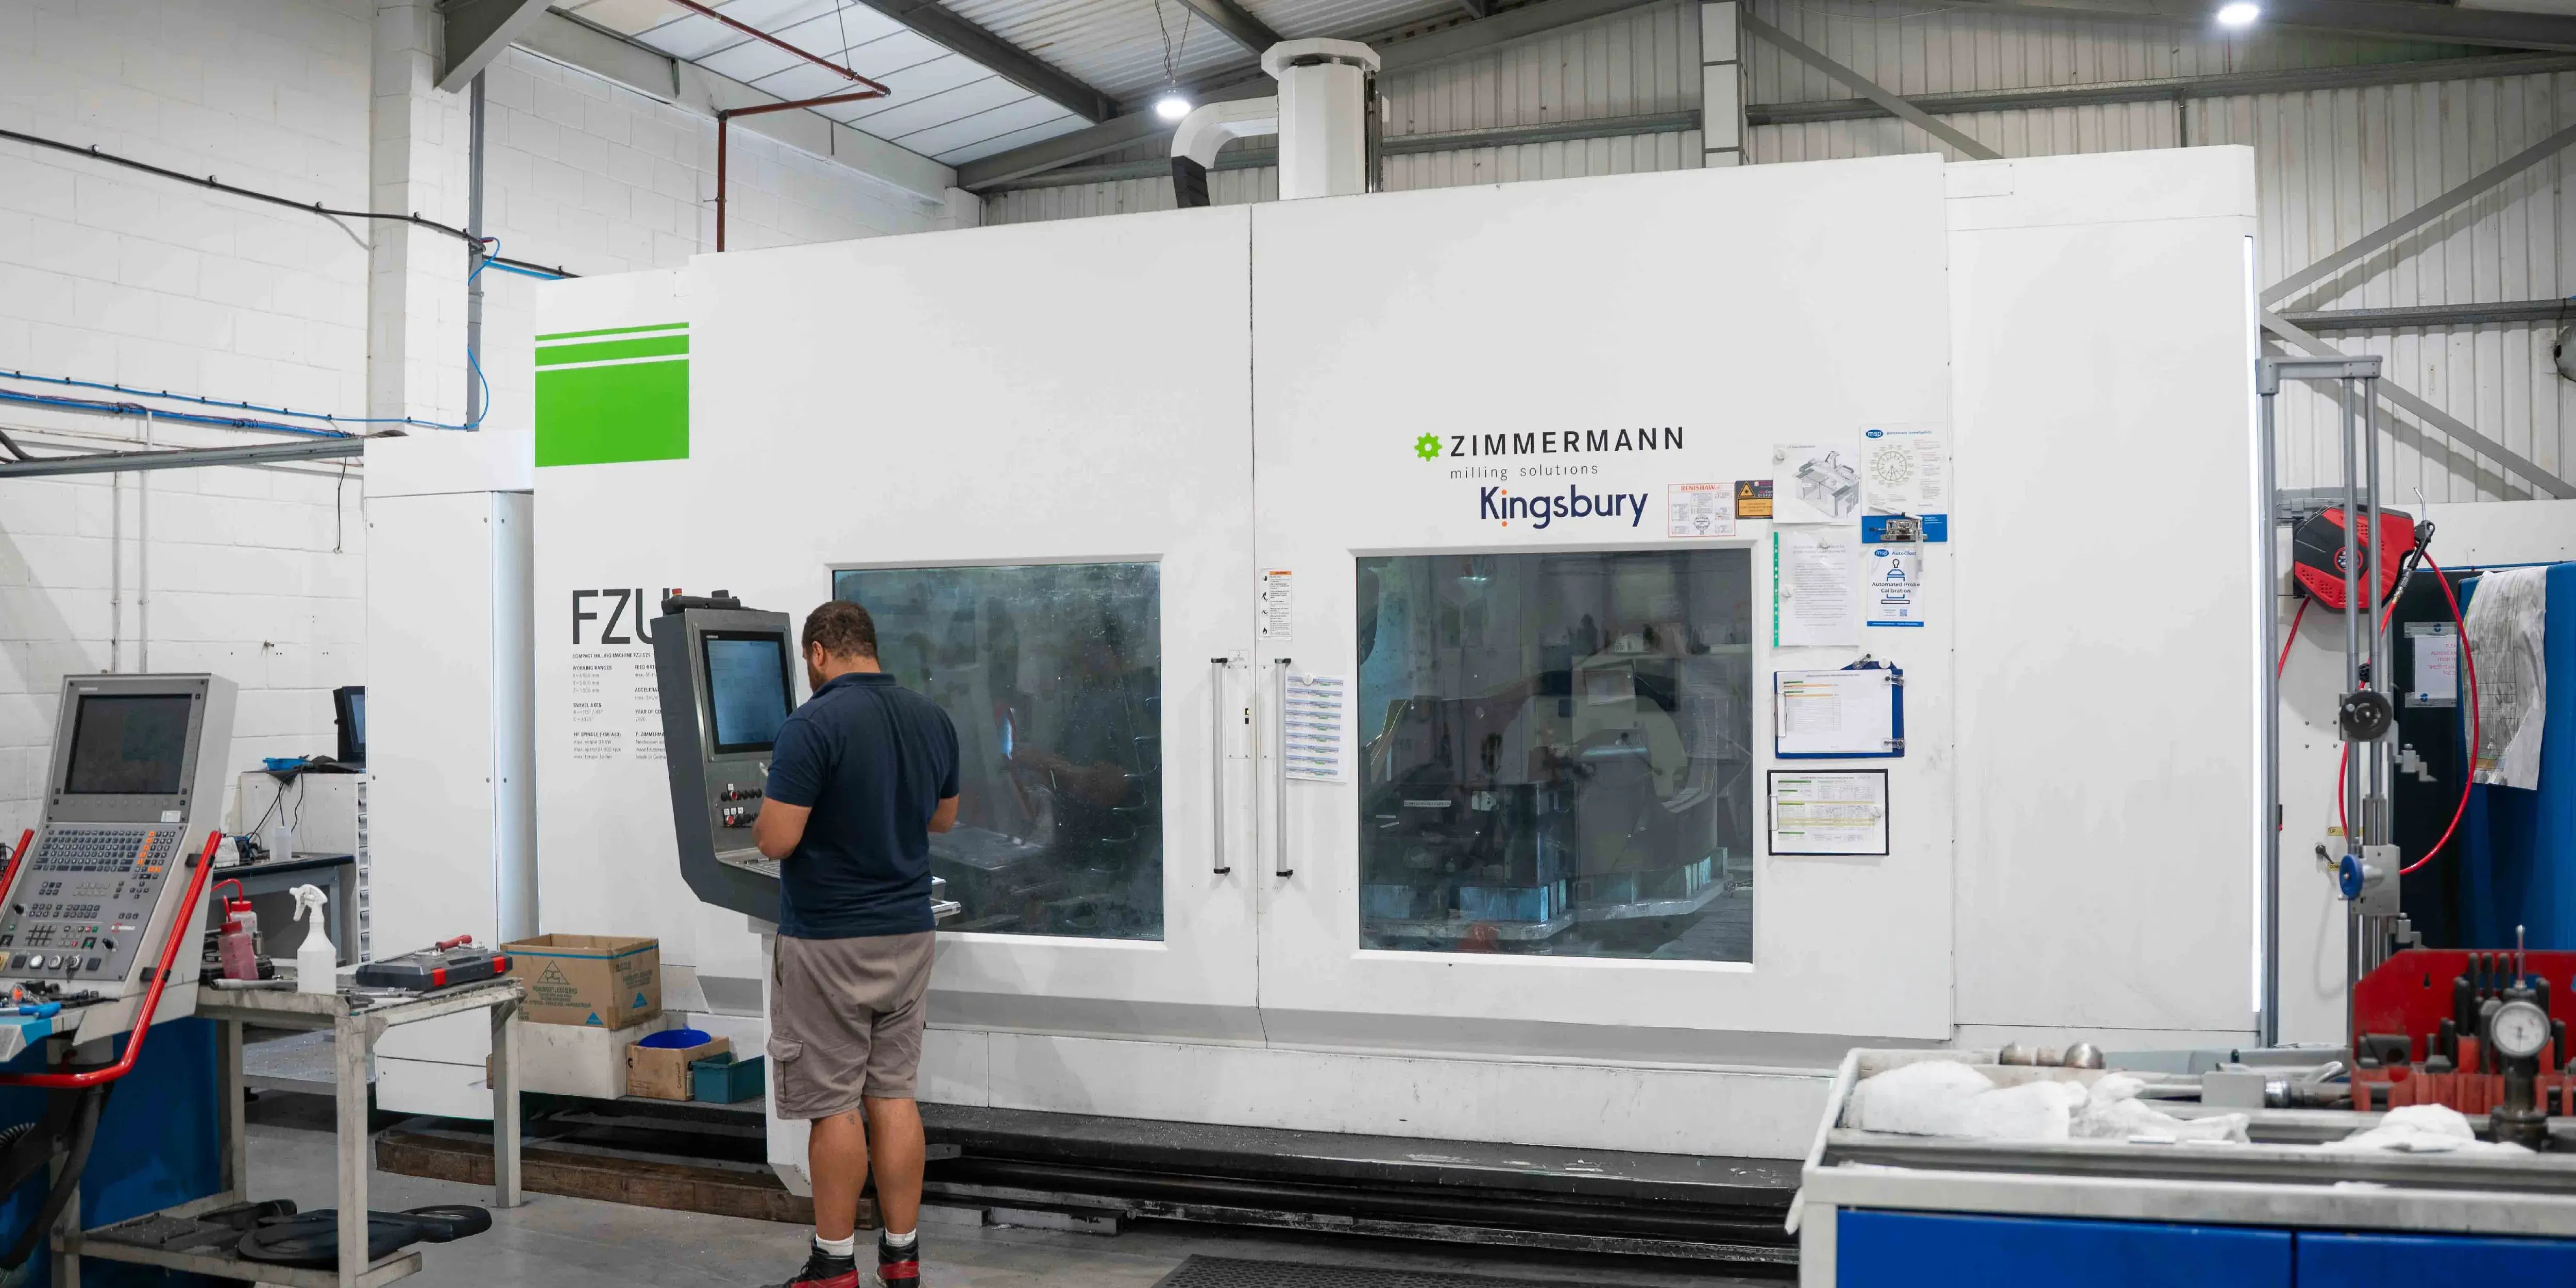
This outlook led GTR to introduce MSP PerfectPart onto its Zimmermann FZU machine. Consisting of three products, AutoClock, NC-Checker and NC-PartLocator, MSP PerfectPart is a suite of metrology products designed to eliminate manual error throughout the CNC machining process.
AutoClock forms the first part of the process, removing the requirement for GTR to use slip gauges within its probe setup routine.
AutoClock automatically calculates the work offset for the artefact which will then be used to calibrate the probe, and this measurement is automatically uploaded to the controller to reduce the risk of manual error occurring at this critical stage.
Steven advocates: “It’s never easy calibrating a probe, but with AutoClock a lot of the manual work has been removed, so the outcome is much more accurate and repeatable”.
To address concerns around unknown machine performance, NC-Checker was implemented next into GTR’s process, and the software is now run monthly on the machine. Steven describes how it works: “NC-Checker gives us a clear indication of the machine’s health and highlights if there’s anything that could cause issues when machining our parts”.
“We always run a full NC-Checker Benchmark to look at everything from the axes and repeatability through to probe health. It’s not about fault-finding, it’s about prevention so we’re safe in the knowledge that the machine is producing the best possible parts”.
Steven Davis, GTR Lead Machine Shop Engineer
NC-Checker also tracks the geometric performance of the machine over time, enabling GTR to monitor if the machine is going to drift out of tolerance and plan in preventative maintenance to get the machine back within the specific parameters.
Steven says: “NC-Checker’s monitoring capability also means temperature fluctuations are no longer as much of an issue as we can track any errors creeping in before they become a problem”.
The final element, NC-PartLocator, has become vital for GTR’s part setup process, removing the need to make manual adjustments to get an accurate setup. NC-PartLocator instead uses 5-axis probing to measure the parts on the machine and generate an accurate best fit alignment in six degrees of freedom. The metrology software accounts for any discrepancies, for example in GTR’s case, part deformation, and automatically uploads the corrected alignment to the controller, removing all misalignment errors.
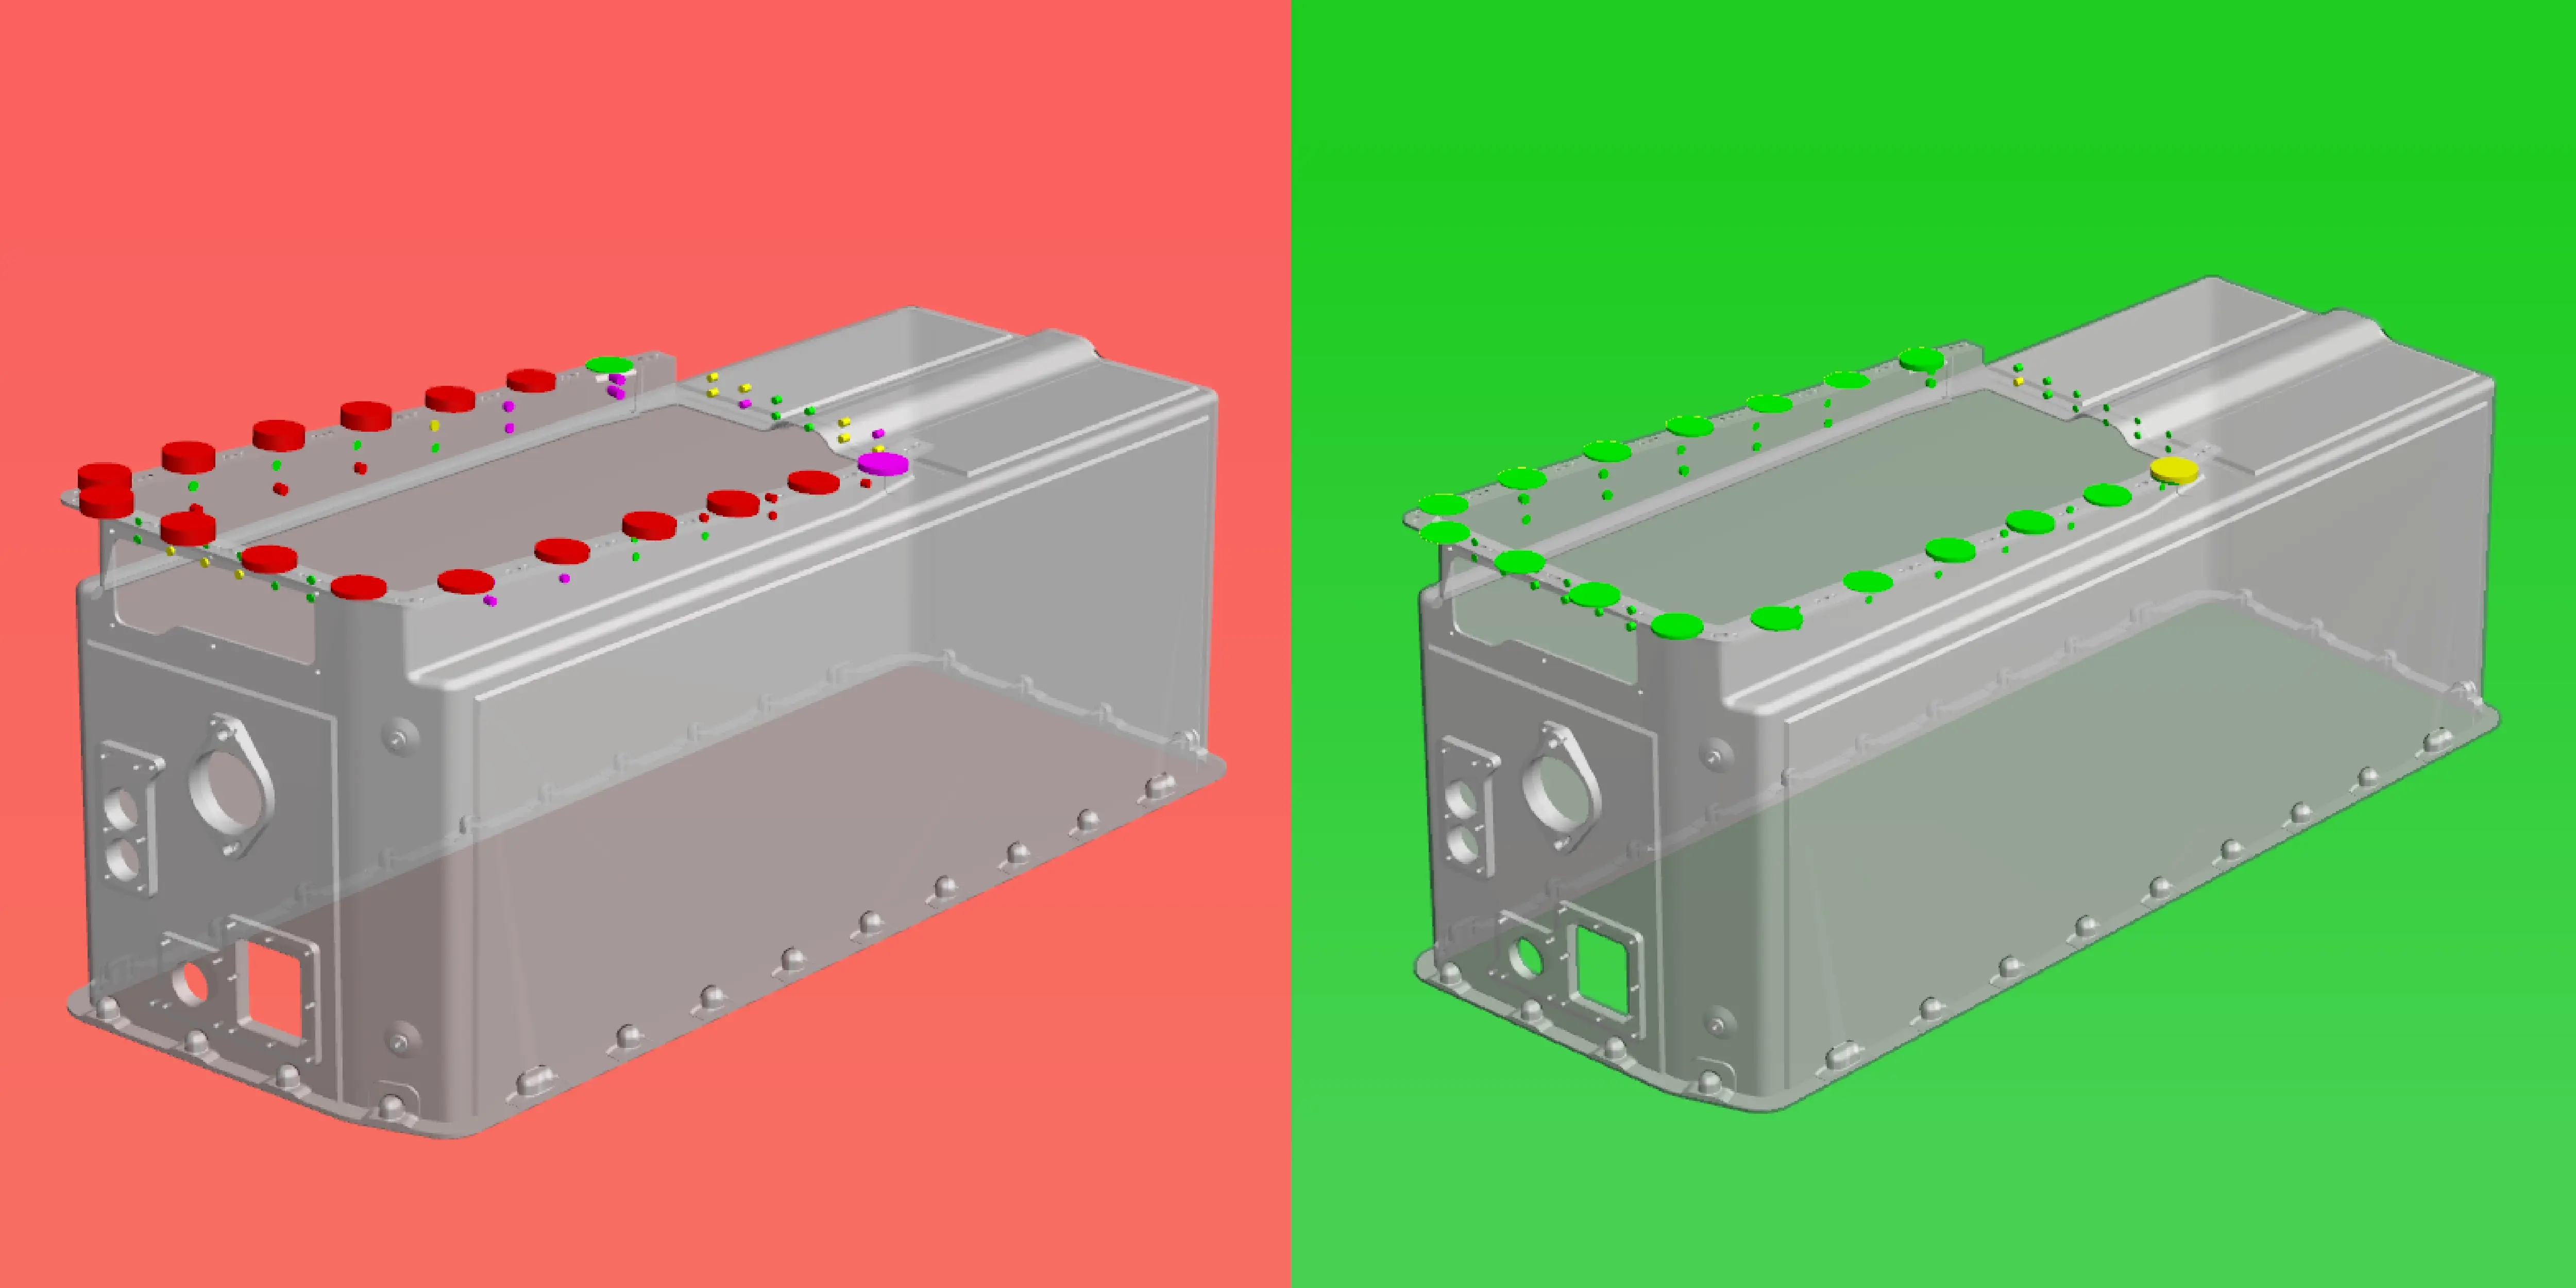
Steven also refers to how this has helped GTR’s fixturing: “Because we no longer need to use the fixture to locate the part, we’ve created a reusable ‘plug-and-play’ type scenario. It means we don’t have to create a fixture from the ground up each time. We just place it on the machine and probe the part with the confidence that the software will work out where it is”.
GTR also uses NC-PartLocator for in-process measurement, re-probing parts to ensure there has been no movement throughout the process, giving the team confidence in their workholding.
Steven summarises: “With NC-PartLocator, you can put a part on the machine, press go and get your parts underway. The data gives us complete confidence that what we’ve got is correct. It’s a game-changer, I never want to set up another race chassis without it”.
Result
MSP PerfectPart’s introduction has exceeded GTR’s expectations, with the positive impact of the software being felt across multiple areas of the business.
Using NC-Checker as a pre-machining ‘sanity check’ has been invaluable. Steven explains: “We were lucky, as NC-Checker uncovered an issue in the C-axis of the machine just before it was due to be laser aligned. Thankfully, a Benchmark had been completed beforehand, so I could factor out the error within the kinematics and stop it from causing any issues. It’s a perfect example of prevention being better than a cure”.
Within the machining process, GTR’s part setup routine has been reduced by 10 hours per part following the introduction of NC-PartLocator. Steven comments: “The reduction in time, along with the stabilisation and repeatability of the setup, has been a godsend on recent projects. We have been able to meet customers’ tight deadlines whilst delivering a product they can rely on to go racing with”.
This level of reliability is becoming increasingly important, with customers looking for greater reassurance than ever before, making GTR’s investment in MSP PerfectPart vital. Steven says: “At the end of the day, it’s the customer’s part, drawing and specifications so we want to ensure they’re happy. MSP’s reports allow us to compare our results with the customer scans and demonstrate we’ve got it as good as it can be”.
This transparency has become a powerful tool when tendering for new work, with MSP now forming part of GTR’s USP. Tom states: “Having MSP PerfectPart gives me the confidence when approaching new tenders, especially high-risk projects. I know we’ve got the tools to iron out any issues, and I can prove both the consistency and quality of supply”.
“Within this sector, there are few areas where significant improvements and savings can be realised, but MSP has found them. You don’t expect this level of innovation, so it’s been a very welcome surprise”.
Tom Hay, GTR Group Business & Operations Development Manager
Future
The increased capability and reliability GTR has achieved with MSP PerfectPart has already attracted a greater volume of work, enabling the company to expand production, with MSP being included in GTR’s future development plans. Tom explains: “We initially considered outsourcing the work but, with our improved capabilities, it quickly became a no brainer to increase operations in-house and avoid the risk of managing an external supply chain”.
As customers’ expectations continue to rise, GTR is also actively engaging in R&D projects to stay ahead of the game alongside its use of MSP PerfectPart. “Technology is always moving forward”, Tom adds, “and as soon as you reach a certain level of accuracy, it naturally becomes the new baseline. We want to stay ahead of that curve and make sure we can continue to go above and beyond for our customers”.
By combining advanced metrology with a proactive approach to innovation, GTR is not only reinforcing its position as a reliable component manufacturer but also helping drive the industry forward in the pursuit of ultimate part accuracy. As expectations continue to evolve, MSP PerfectPart will remain central to meeting them with confidence and ease.
More case studies
MSP helps Formula 1 team reduce part setup by 9.5 hours
A leading F1 team used products from MSP PerfectPart to reduce their part setup time from 10 hours to 38 minutes.
More case studies
Production time cut from 20 weeks to 3 days for Leonardo
MSP PerfectPart allowed Leonardo to machine complex tiltrotor blades with extreme distortion and cut production time to 3 days.
More case studies
SST now producing 700% more parts per week
SST is now manufacturing 7 times more parts per week and reduced its part setup time from 4 hours to 25 minutes.
More case studies
Part setup cut from 5 hours to 10 minutes for 3T-am
3T-am now produces right-first-time parts and leaves the machine to run overnight for full 24/7 lights-out automation.
More case studies
100% productivity increase for castings manufacturer
Doncasters has also been able to simplify fixturing and bring work in-house to aid production.
More case studies
Pentaxia eliminates 100% concession rate
Pentaxia also reduced production time for a set of parts by 50%, from 40 hours to 20 hours.
More case studies
Quickstep halves setup time and reduces rework by 75%
Quickstep's CNC machine assessments have also been cut by 96%, from 2-4 days to 1-2 hours.
Be in a case study.
If you’ve had impressive results and want to be involved in your own case study, we want to hear from you! It’s a great way to shout about the collaboration between our great companies.